
 Tiếng Việt

Manufacture
FARMILA is a leading Vietnamese enterprise in the field of rice processing and storage equipment. Our standout feature is that FARMILA directly designs and manufactures industry-standard square silos and various auxiliary equipment used in post-harvest processes. Each product is developed through in-depth research, incorporating advanced technology combined with local expertise to ensure compliance with the industry’s stringent standards while being suitable for Vietnam’s climate and farming practices.

Research, Design, and Manufacture Process
FARMILA’s manufacture process begins with research and development (R&D), led by a team of experienced engineers. Each product is designed by combining advanced technology with local practical needs, ensuring real-world applicability. Manufacture takes place at FARMILA’s factory with modern equipment and skilled personnel. The process is subject to strict quality control, ensuring that products meet industry standards, are durable, stable, and highly accurate.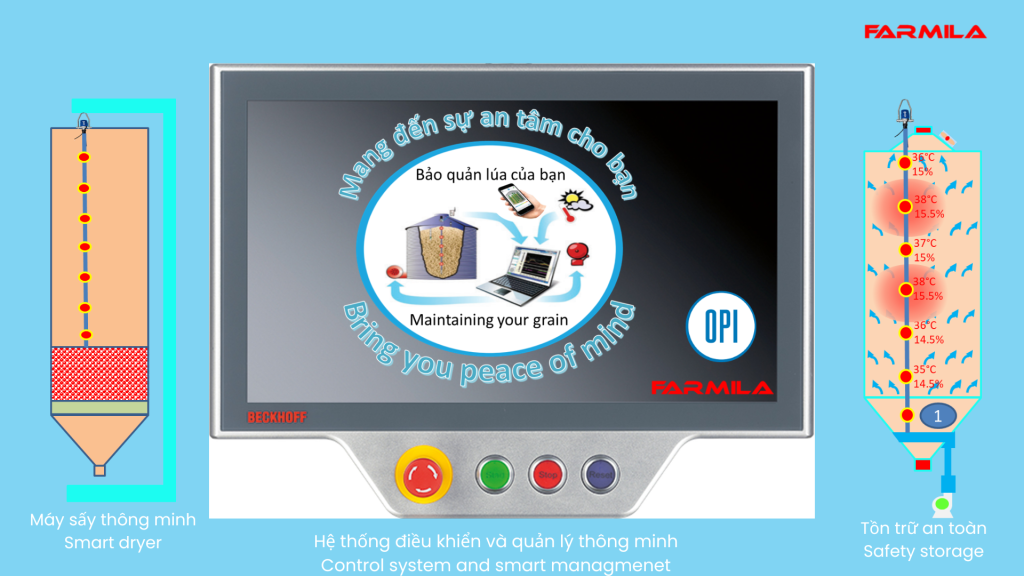
Practical Contributions to Agriculture
FARMILA’s solutions have been applied in many key rice production areas. With modern systems, businesses can proactively store, minimize losses, and optimize production efficiency. Through this, FARMILA plays a significant role in the industrialization of Vietnamese agriculture.

Key Products and Auxiliary Equipment
- Industry-standard square silos: Capacity ranging from 140 tons/module to thousands of tons. Corrosion-resistant, equipped with temperature and humidity control systems.
- High-capacity rice dryers: Including circulating dryers with 40–50 tons/batch and horizontal static dryers with 50 tons/batch.
- Conveyor and bucket elevator systems: High capacity, flexible operation, supporting automated handling of large volumes.
- Automated control systems: Integrated with PLC/SCADA, managing the entire production line, supporting IoT connectivity and remote control.

Flexible and Easily Integrated into Modern Systems
- FARMILA’s products feature an open structure, making them easy to expand and integrate. Customers can select equipment from other brands to integrate into the overall system, and FARMILA will support synchronization to ensure efficient operation. All control systems are compatible with ERP, SCADA, or IoT platforms.
Key Advantages of FARMILA Products
- High durability, stable operation, adaptable to harsh conditions.
- Cost savings in investment and operation, reducing post-harvest losses.
- High automation, intelligent monitoring, supporting remote operation.
- Flexible design, easy to upgrade and integrate with other systems.
- Suitable for the domestic market, user-friendly, with prompt technical support.